 WhatsApp Us Now

Buying a water cart means choosing the company that builds it. The factors that matter: engineering, certified quality, compliance, and real support.
It’s easy to shop for a water cart the way you’d shop for a commodity: compare tank sizes, compare prices, pick one. But a water cart is a custom-engineered asset that has to survive years of punishing work, and the thing that decides whether it does is the company that built it.
Get the manufacturer right, and you get a cart that performs safely, holds its value, and is supported for its full life. Get it wrong and you inherit the consequences: cracked tanks, compliance gaps, and a supplier who’s hard to reach when something fails on a remote site. So the real decision isn’t which water cart to buy. It’s which engineering company to trust with the build. These are the factors worth weighing before you commit.
Do they engineer, or just assemble?
The first question separates the serious manufacturers from the rest. Some suppliers stock and sell standard units. A genuine engineering company designs and builds to your requirements, matching the tank to your chosen chassis, your site conditions, and your operational demands.
Look for a company that consults before it quotes, one that establishes your strategic, operational, and budget requirements first, then recommends and builds around them. That order matters. A cart engineered to suit your prime mover, your haul distances, and your compliance needs will always outperform a generic unit adapted to fit. If a supplier leads with models and prices before understanding your operation, that tells you what you’re getting.
Certified quality and mine-spec compliance
For anyone signing off the spend, quality can’t rest on a salesperson’s word. It needs to be systematic and documented. Check that the manufacturer builds under a recognised quality management system; ISO9001:2015 certification means quality is consistent and repeatable across every build, not dependent on who happened to be on the floor that week.
Compliance is the other half. A water cart bound for a mine site has to meet strict safety requirements, and the best manufacturers build these in as standard rather than retrofitting them: isolation points, emergency stops, compliant lighting, ROPS, and safe access. Ask whether a cart arrives mine-spec compliant off the line, and whether the compliance is documented. For procurement, that documentation is what removes risk from the purchase.
Australian-made and built for local conditions
Where a water cart is built shapes how well it copes and how easily it’s supported. A cart designed and manufactured in Australia is engineered from the outset for local conditions, extreme heat, abrasive dust, corrugated haul roads, and remote operation, rather than adapted from an imported template built for somewhere else.
Local manufacturing also means local support. Parts, service, and technical help are close at hand rather than an ocean and a shipping delay away. When a cart is down, that proximity is the difference between a quick fix and a long wait.
Range and fleet capability
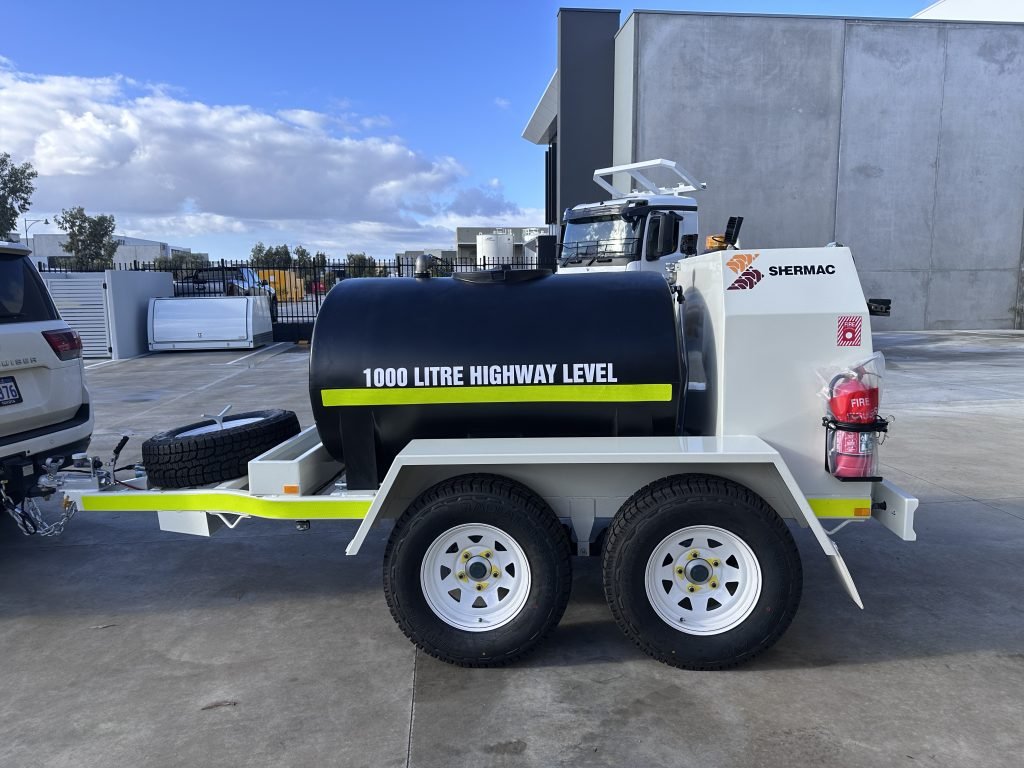
If you run or plan to run more than one water cart, the breadth of a manufacturer’s range matters more than it first appears. A company that builds across the full spread, from compact truck-mounted carts through to large rigid and articulated haul-truck builds, can supply your entire fleet with consistent engineering and a single point of accountability.
That consistency simplifies standardisation, servicing, and operator familiarity across the fleet, and it means one relationship instead of several as your needs change. A supplier who only covers one part of the range forces you to juggle multiple vendors as you scale.
Track record and proof
Claims are cheap. Evidence isn’t. The strongest signal a water cart engineering company can offer is a track record with demanding operators. Ask who’s running their carts and in what conditions.
A manufacturer whose equipment is trusted across Tier 1 operations, including BHP, Rio Tinto, FMG, and Mineral Resources, has been tested against the highest standards in the country. Referenceable performance at that level, backed by customer testimonials and case studies, tells you far more than any brochure. If a supplier can’t point to proven work in conditions like yours, treat that as a gap.
Support after the sale
The purchase is the start of the relationship, not the end, and the factor most often underestimated is what happens once the cart is in service. Check the warranty terms; an industry-leading warranty on manufactured components signals a company that stands behind its build, and confirm that parts supply and technical support are available for the full lifecycle of the equipment.
Lead times matter too. Ask about build capacity and delivery timeframes upfront, especially if the cart is tied to a project schedule. A manufacturer who’s clear about lead times and backs the equipment long-term’ll still be there when you need them, which is exactly when it counts.
Frequently asked questions
What’s the difference between a water cart supplier and a manufacturer?
A supplier typically stocks and sells standard units, while a manufacturer designs and engineers carts to your requirements, matching tank, spray systems, and mounting to your chassis and site. For custom or mine-spec needs, an engineering manufacturer builds a water cart tailored to your operation rather than a generic one that’s just adapted to fit.
Why does ISO9001:2015 certification matter for a water cart?
It means the manufacturer works to a recognised quality management system, so every cart is built to a consistent, documented standard. For procurement and compliance, that documentation reduces risk and gives you confidence the build quality isn’t dependent on chance.
How important is local manufacturing for a water cart?
Very, for two reasons. A cart built in Australia is engineered for local conditions from the start, and local manufacturing means parts, service, and support are close at hand. That proximity keeps downtime short when repairs or spares are needed.
The bottom line
Choosing a water cart is choosing the company behind it. Weigh engineering capability, certified quality, compliance, local manufacturing, range, proven performance, and long-term support, and you’ll end up with a cart that earns its keep rather than one that costs you later. Judge the manufacturer, and the right cart follows.
To see what a purpose-built, mine-spec build looks like across the full range, explore Shermac’s water cart range.


